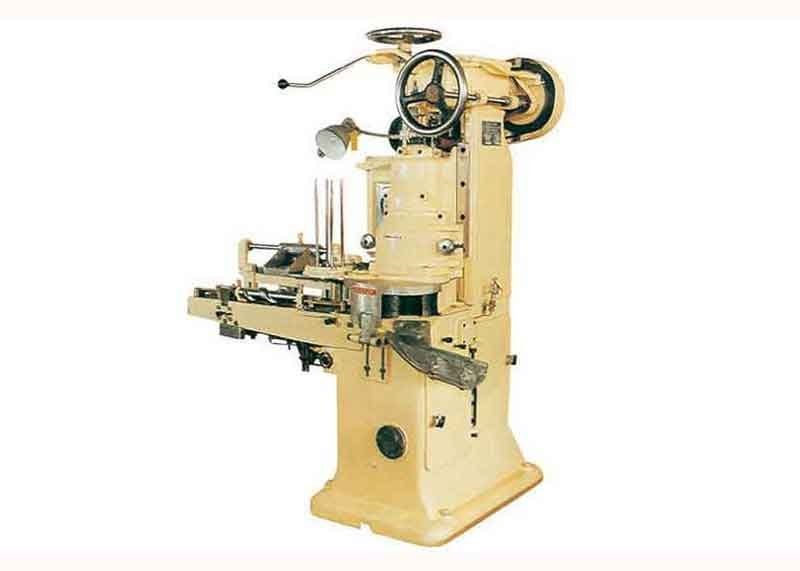
Filling, closing & capping
Vacuum can seamer
Model: GHFJ-2
Seams a tin can under vacuum, so the headspace is oxygen-poor before the retort.
Tell us your product, target output and packaging requirements.
Product overview
The can is lifted into a vacuum chamber, the lid is placed, and two seaming rollers roll the curl into the can flange. Vacuum in the chamber is drawn before the seam closes, which removes the headspace air that would otherwise oxidise the product in the retort. Seam dimensions are set with a gauge and checked at start-up; the machine is the closing step on a tin-can line and pairs with the following gear-pump filler upstream.
Technical specifications
Reference information from the current equipment catalogue. Final configuration, output and supply scope are confirmed for your project.
| Model | GHFJ-2 |
|---|---|
| Type | Automatic vacuum can seamer |
| Seaming | Two-roller, first and second operation |
| Can sizes | By change parts (diameter and height) |
| Vacuum | Chamber vacuum, adjustable |
| Material | SUS304 frame and chamber |
| Lead time | 45–60 working days |